Skip to content
ArcSteel.Technology

Applications

From liquid hot metal to finished ingot

Every stage has its own failure mode and its own material that fixes it. These are the problems we see come up again and again in the plants we supply.

  1. 01

    Hot metal pretreatment

    The problem

    Hot metal sits in the ladle or torpedo car losing temperature before it reaches the converter. Every degree lost has to be paid for later in the heat.

    How we deal with it

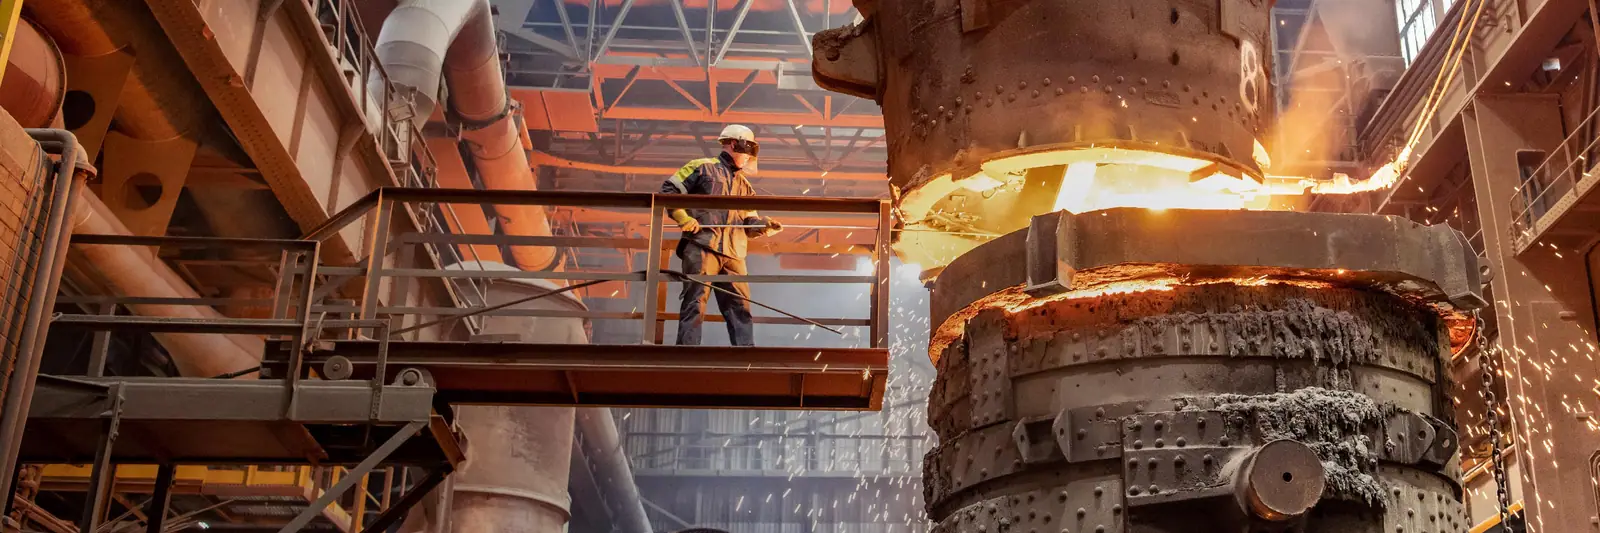
    A Hot Metal Ladle Covering Flux forms an insulating layer on the surface, cutting radiation losses and keeping the metal hot until it is charged.
    Products used here

  2. 02

    Converter steelmaking

    The problem

    Slag that is too viscous resists desulphurisation and holds inclusions, and the operator compensates by adding more lime — which makes things worse and costs money.

    How we deal with it

    A Slag Fluidizer lowers the slag melting point and improves fluidity, so desulphurisation proceeds faster and lime consumption drops.

  3. 03

    Electric arc furnace (EAF)

    The problem

    High power input and long tap-to-tap times make slag control critical. Poor slag practice wastes energy and lengthens the heat.

    How we deal with it

    Fluxing agents tailored to your slag system keep the slag reactive at lower lime addition, shortening the heat and cutting energy per tonne.

    Products used here

  4. 04

    Ladle refining (LF / VD)

    The problem

    During refining and transport, the steel surface is exposed to air and radiates heat away. That means temperature loss, reoxidation and inclusions that never leave the bath.

    How we deal with it

    A Ladle Covering Flux forms a continuous liquid layer that insulates the bath, blocks secondary oxidation and absorbs rising inclusions.

  5. 05

    Continuous casting

    The problem

    The tundish is the last place you can keep the steel clean. Poor cover means heat loss, reoxidation, and nozzle clogging that shows up later as surface and internal defects.

    How we deal with it

    Tundish Covering Flux insulation plus correctly graded Ladle Sand: the bath stays hot and clean, and the ladle opens first time at the caster.

    Products used here

  6. 06

    Ingot casting

    The problem

    Two problems cost money at the same time: surface defects on the ingot skin, and pipe and shrinkage cavities in the riser that force you to crop the top.

    How we deal with it

    Ingot Teeming Flux keeps the steel surface protected and lubricates the mould, while an Exothermic Hot Topping Compound keeps the riser liquid so defects stay in the head and get cropped cleanly.

  7. 07

    Foundry & casting

    The problem

    Risers that freeze too early leave shrinkage porosity in the casting — and that means rejection, re-work and unhappy customers.

    How we deal with it

    Riser exothermic and feeding agents designed for the section size you cast, so the riser feeds the casting properly and solidification stays directional.

Experience

Southeast Asia is our core market

Vietnam, Thailand, Indonesia, Malaysia and Singapore are the markets we ship to regularly. We know how the hot, humid climate affects storage and packing — and we pack accordingly.

Moisture-barrier packing

Lined bags and jumbo bags that keep the product free-flowing on arrival, not caked solid.

Correct documentation

Invoice, packing list and export documents prepared so the container clears without being held.

Support in English and Vietnamese

Technical discussions in English or Vietnamese with the people who actually make the product.

Trial batch before volume

Run a small batch to your specification so you can verify performance before committing to volume.

Tell us which stage is giving you trouble

Describe the symptom — temperature loss, nozzle clogging, surface defects, shrinkage pipe. We will tell you the most likely cause and how to deal with it.

Nanyang Shangli Metallurgical Refractory Co., Ltd. — 河南省南阳市西峡县回车镇石梯村后河组20号